Automotive
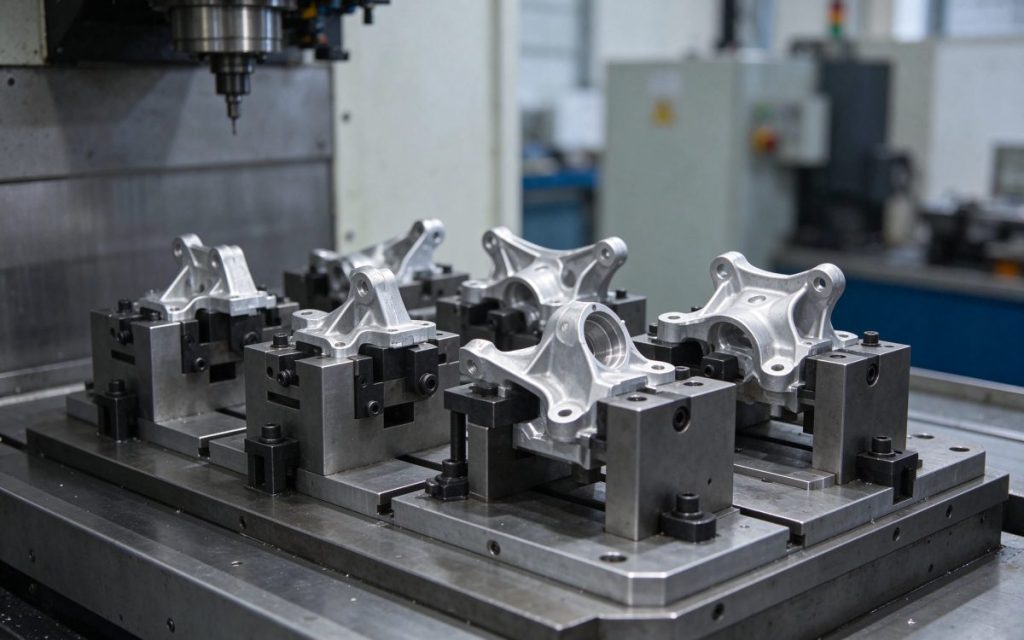
Valve bodies, four-up fixture on a VMC
A four-station fixture that turned a single-part valve body job into a four-part cycle, with the operator loading outside the machine.
Read caseCASE STUDY Automotive
An aluminium steering knuckle that used to need two setups now leaves one vertical machining centre complete, with hole position held across the batch.
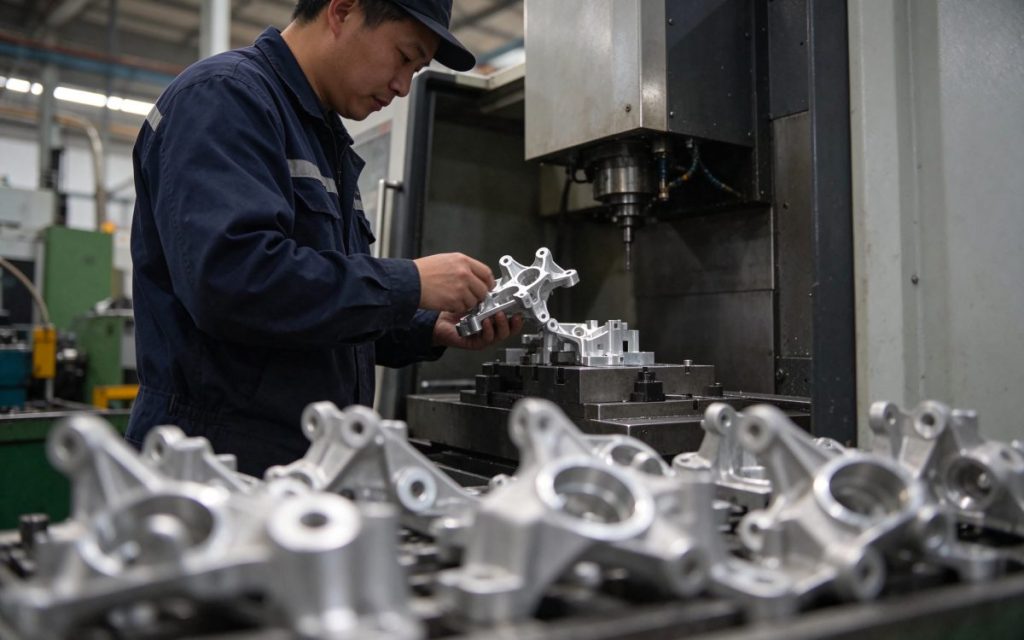
The customer was machining this knuckle on two separate fixtures — one for the mounting face, one for the bearing bore — and re-datuming between them. Hole position drifted, and every batch needed a manual check on the CMM.
We proposed a single fixture holding four parts on a tombstone, with the bore and the mounting face machined in the same cycle. Tooling was kept to eight cutters, all in the standard magazine, so no special tooling order was needed.
After the trial cut the shop ran 40 parts and measured every one. Bore-to-face position stayed inside 0.02 mm, and the second operation disappeared from the routing. The customer has since ordered two more machines for the same cell.
MORE CASES
Automotive
A four-station fixture that turned a single-part valve body job into a four-part cycle, with the operator loading outside the machine.
Read case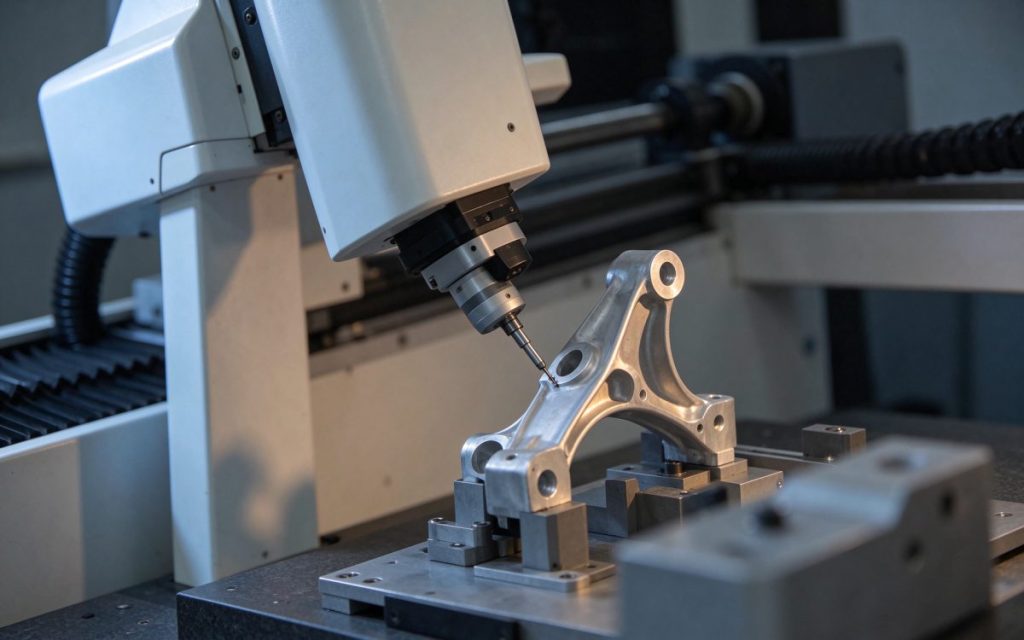
Automotive
A CMM station beside the cell that turned first-article inspection from a two-day wait into a 20-minute check.
Read case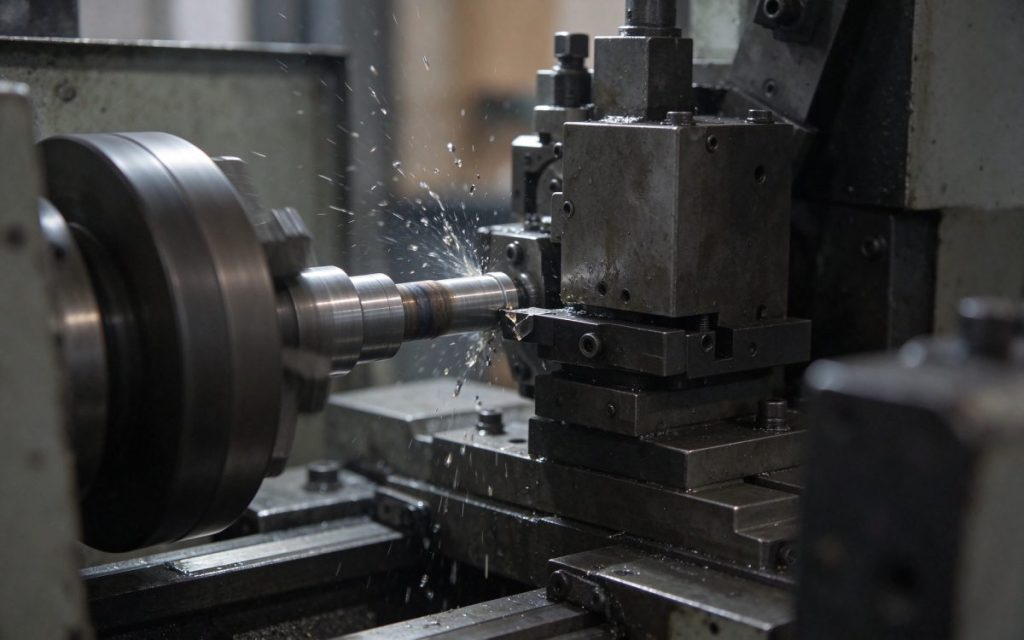
Automotive
A 420 mm hydraulic piston rod that used to travel between a lathe and a mill now comes off a turn-mill centre complete, thread and flats included.
Read caseTECHNICAL DATA SHEET
Series datasheet · PDF, 1 page
Tell us where to send follow-up questions and the PDF opens immediately. No newsletter, nothing shared.
Used to follow up on this request only. See our privacy policy.