Automotive
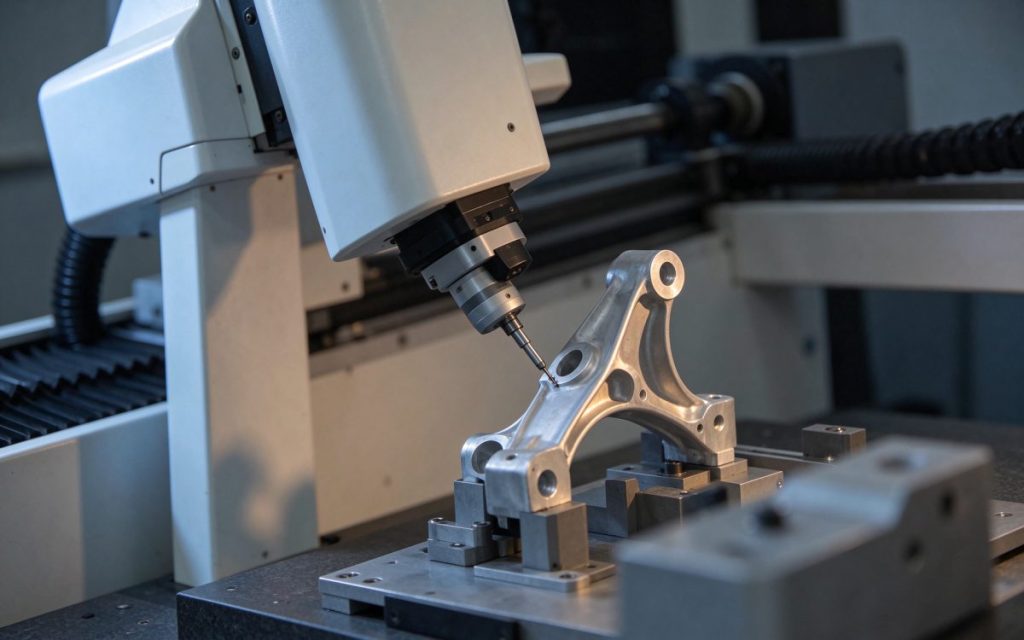
First-article checks moved to the machine
A CMM station beside the cell that turned first-article inspection from a two-day wait into a 20-minute check.
Read case
Automotive
A CMM station beside the cell that turned first-article inspection from a two-day wait into a 20-minute check.
Read case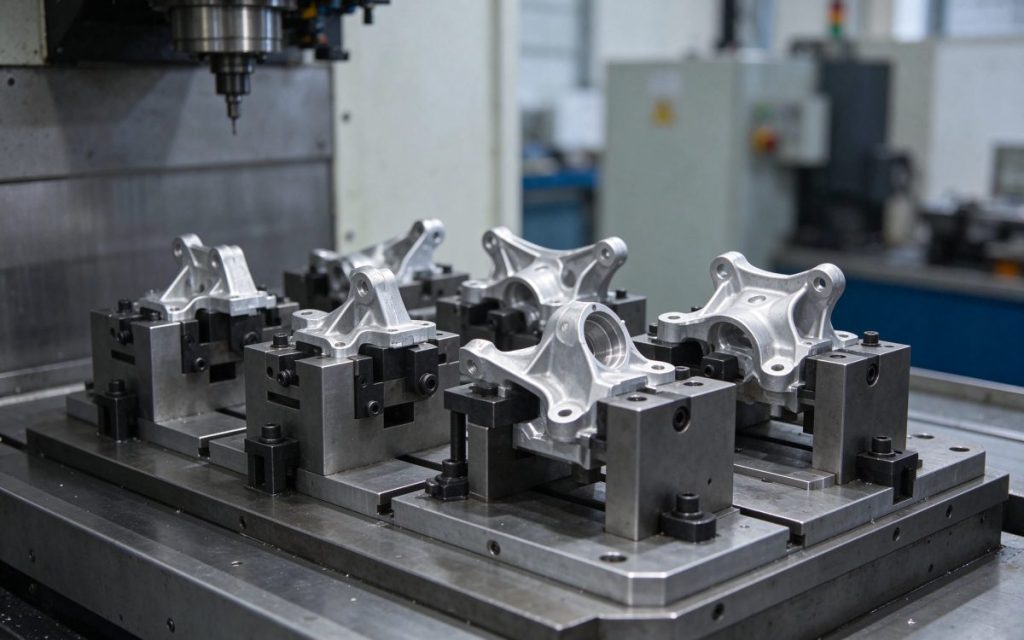
Automotive
A four-station fixture that turned a single-part valve body job into a four-part cycle, with the operator loading outside the machine.
Read case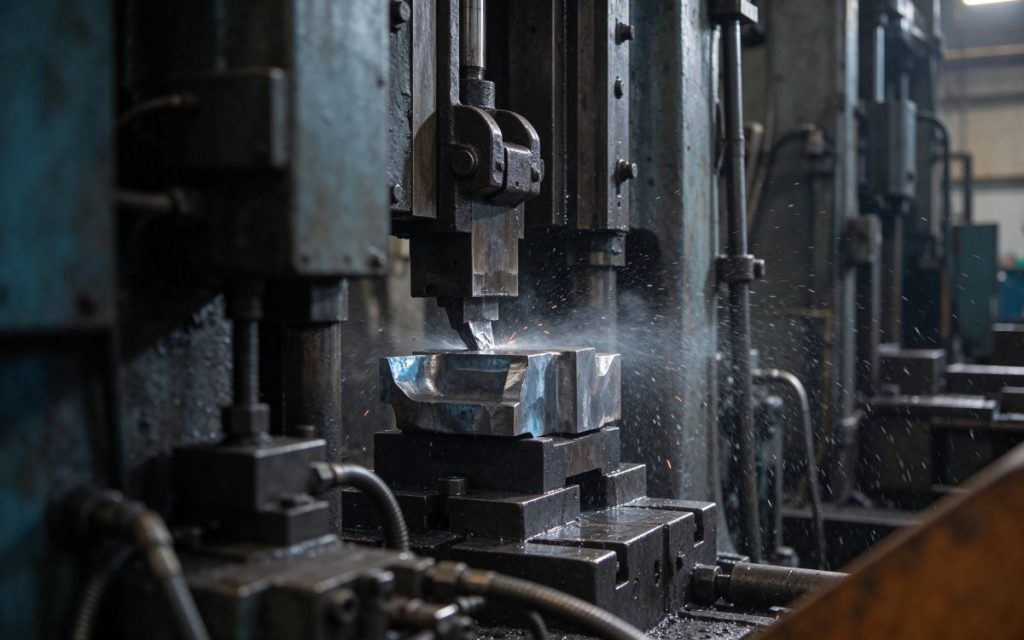
Mould & die
Hardened die inserts that used to be ground after milling now come off the machine with the parting line inside tolerance.
Read case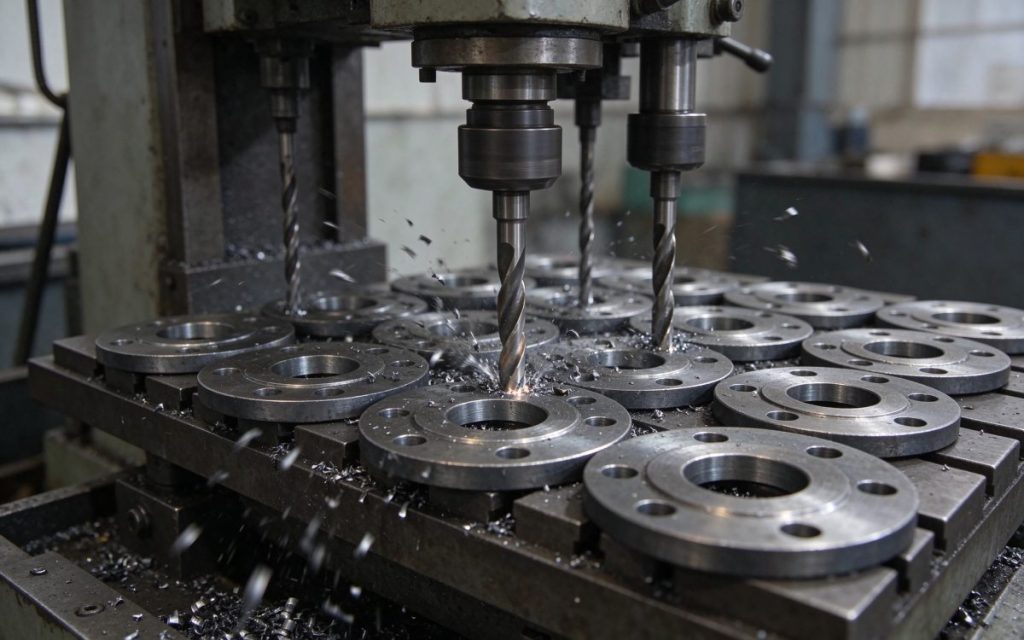
Mould & die
Eight steel flanges with six bolt holes each, drilled and countersunk in a single cycle on a vertical drilling machine.
Read case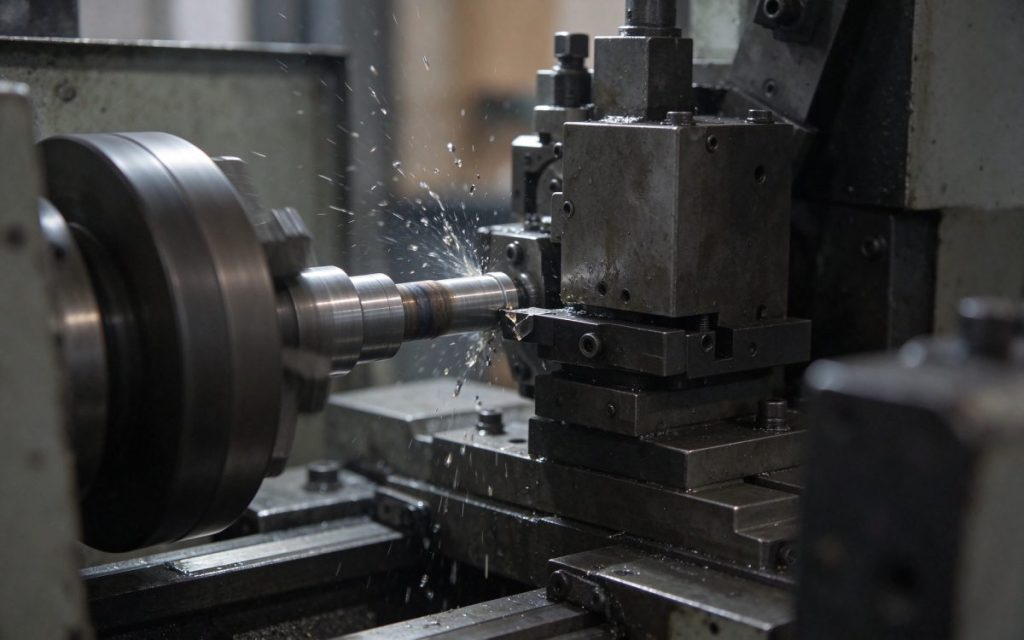
Automotive
A 420 mm hydraulic piston rod that used to travel between a lathe and a mill now comes off a turn-mill centre complete, thread and flats included.
Read case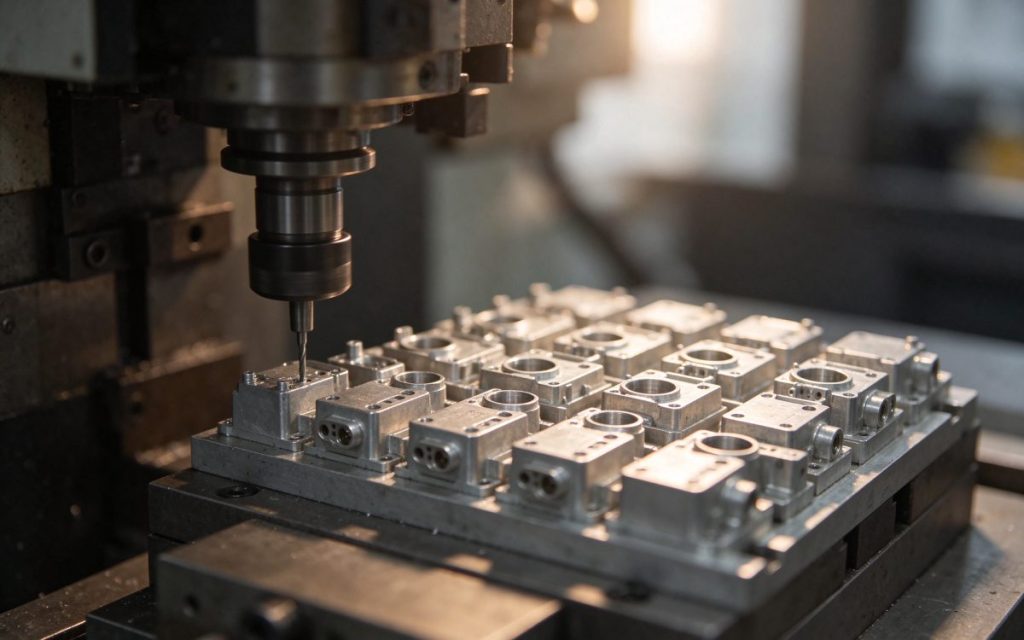
Electronics
Small aluminium connector shells with three bores each — 24 parts on one plate, tapped in the same cycle.
Read case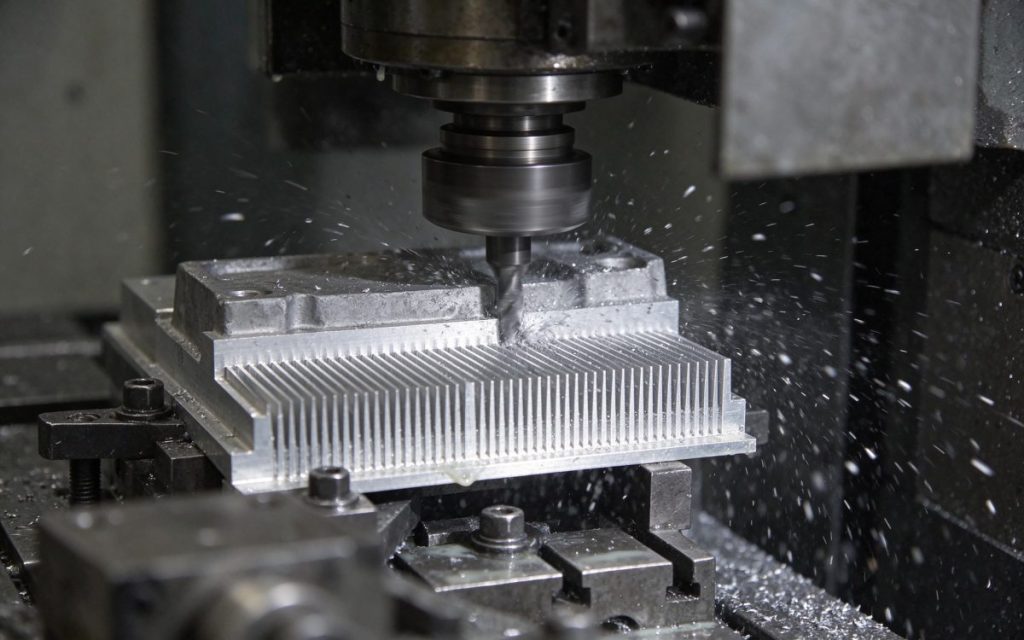
Electronics
A 180 × 120 mm extruded heatsink base needed the fin roots cleaned and the mounting face flat within 0.05 mm — done in one clamping on a vertical mill.
Read case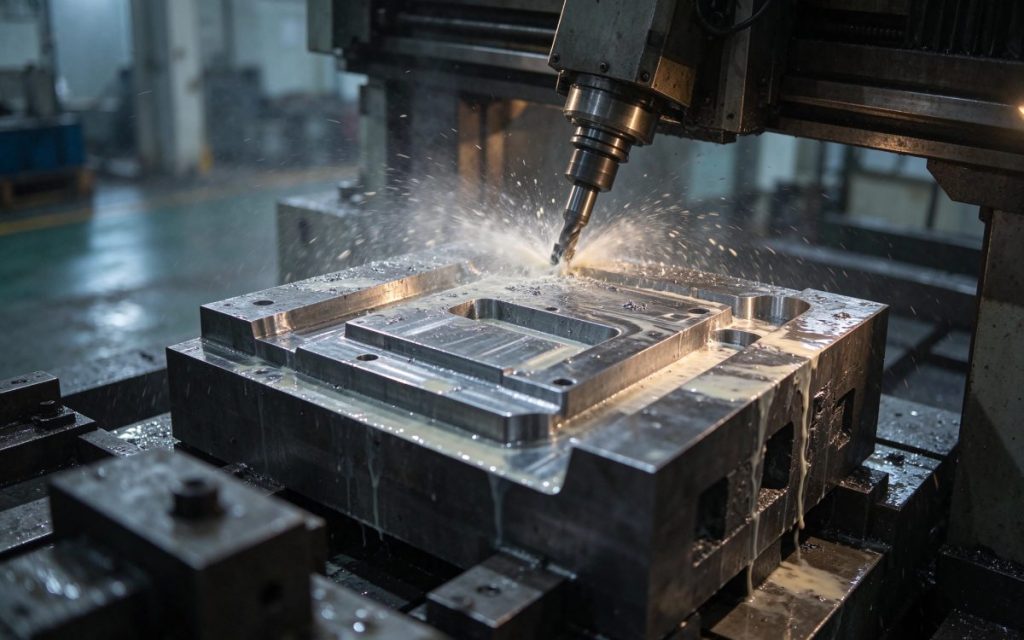
Mould & die
A 1.2-tonne mould core where roughing and finishing now happen on the same gantry machine, with the contour left to a single finishing pass.
Read case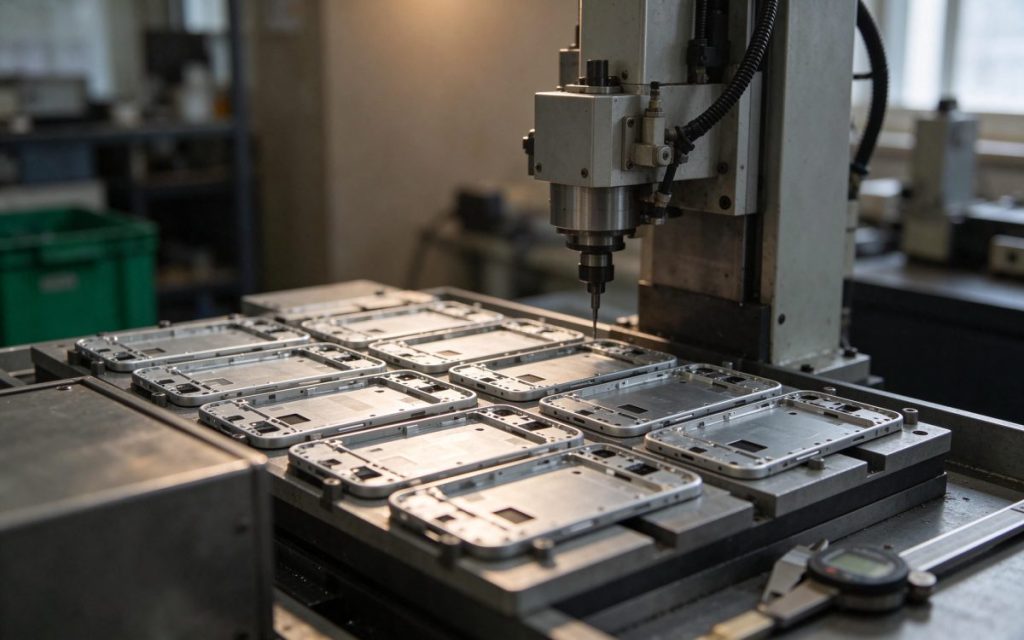
Electronics
Thin-walled aluminium frames with 46 tapped holes each — run on a compact drilling and tapping centre with a repeatable fixture and a fast tool change.
Read caseTECHNICAL DATA SHEET
Series datasheet · PDF, 1 page
Tell us where to send follow-up questions and the PDF opens immediately. No newsletter, nothing shared.
Used to follow up on this request only. See our privacy policy.