Mould & die
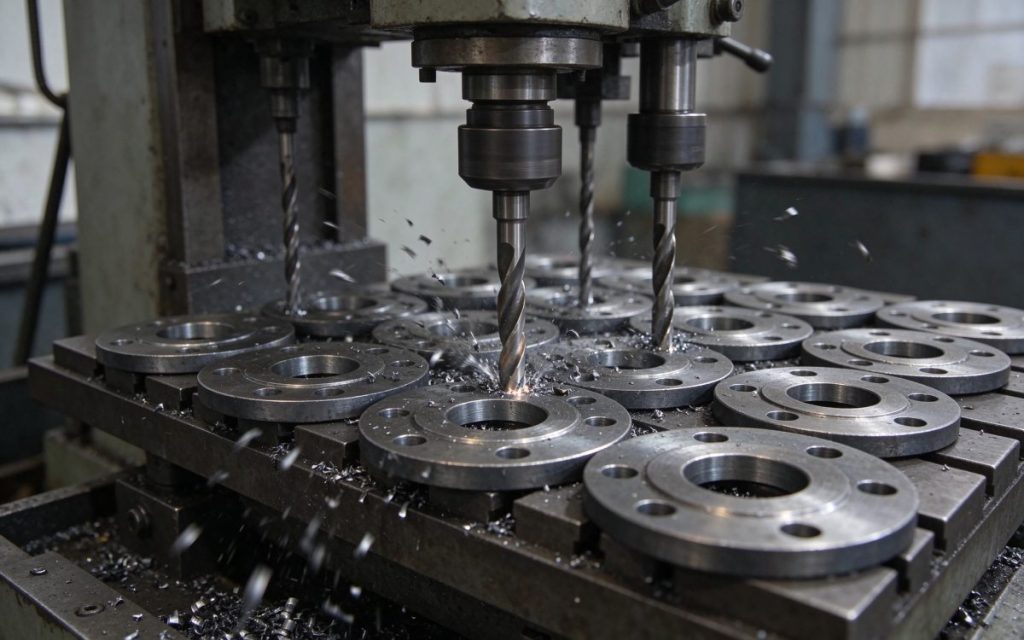
Flange plates drilled in one hit, eight at a time
Eight steel flanges with six bolt holes each, drilled and countersunk in a single cycle on a vertical drilling machine.
Read caseCASE STUDY Mould & die
A 1.2-tonne mould core where roughing and finishing now happen on the same gantry machine, with the contour left to a single finishing pass.
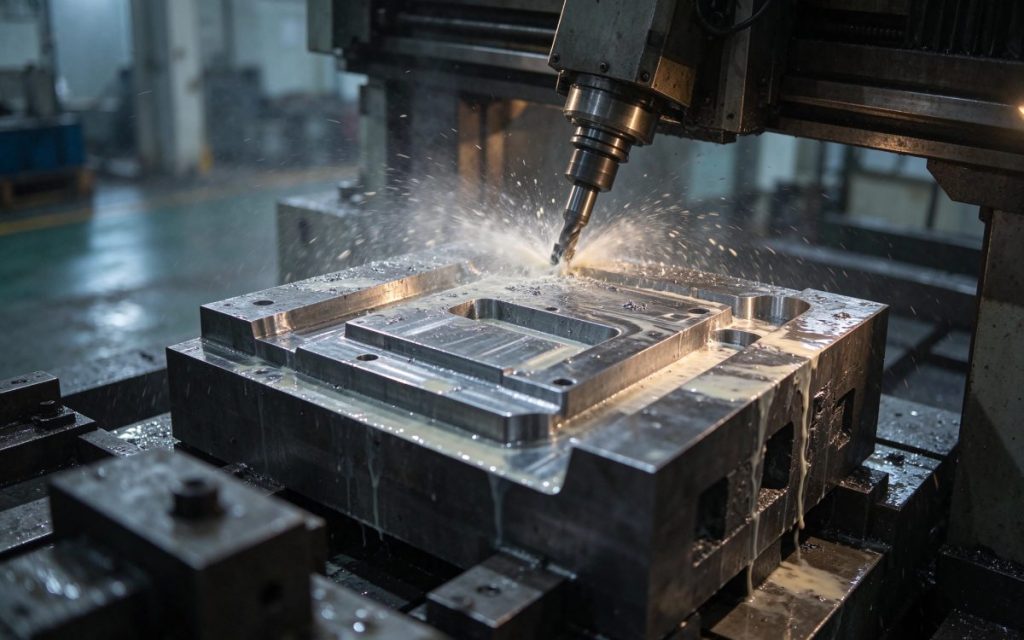
The core used to be roughed on an older bed mill and then moved to a second machine for finishing, which meant a re-clamp and a re-datum for every core. Contour mismatch showed up as a step that had to be polished out by hand.
With the gantry machine the core is roughed, semi-finished and finished in one clamping. The three finishing passes follow a constant step-over, and the operator only checks the depth of the cavity and the parting line before release.
Nine hours per core came off the routing. The shop now books the gantry for finishing work only, and the bed mill handles the roughing of the next core in parallel.
MORE CASES
Mould & die
Eight steel flanges with six bolt holes each, drilled and countersunk in a single cycle on a vertical drilling machine.
Read case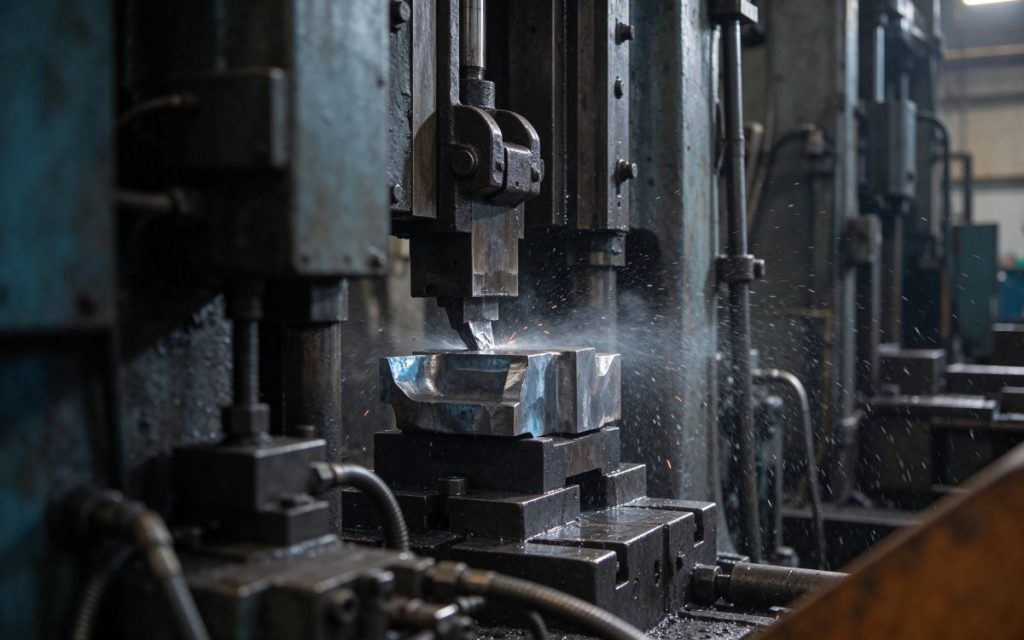
Mould & die
Hardened die inserts that used to be ground after milling now come off the machine with the parting line inside tolerance.
Read case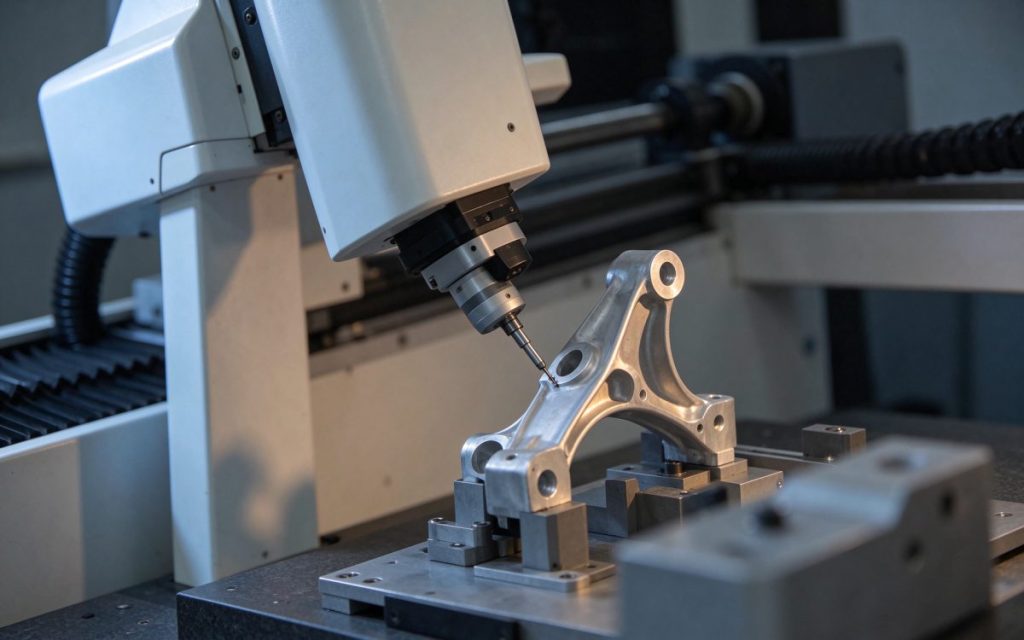
Automotive
A CMM station beside the cell that turned first-article inspection from a two-day wait into a 20-minute check.
Read caseTECHNICAL DATA SHEET
Series datasheet · PDF, 1 page
Tell us where to send follow-up questions and the PDF opens immediately. No newsletter, nothing shared.
Used to follow up on this request only. See our privacy policy.