Electronics
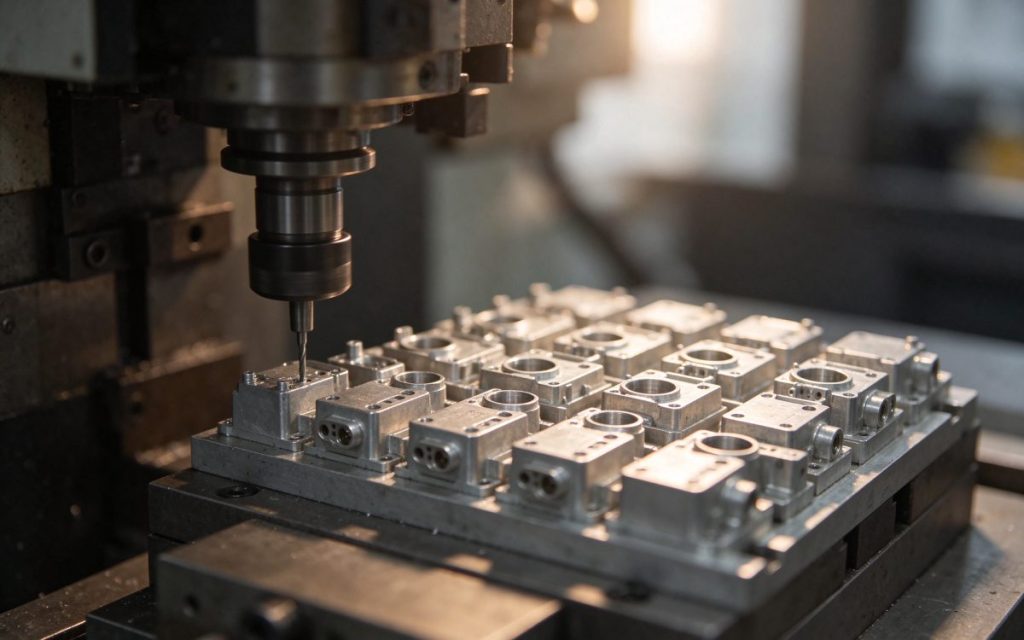
Connector shells, 24 parts per cycle
Small aluminium connector shells with three bores each — 24 parts on one plate, tapped in the same cycle.
Read caseCASE STUDY Electronics
A 180 × 120 mm extruded heatsink base needed the fin roots cleaned and the mounting face flat within 0.05 mm — done in one clamping on a vertical mill.
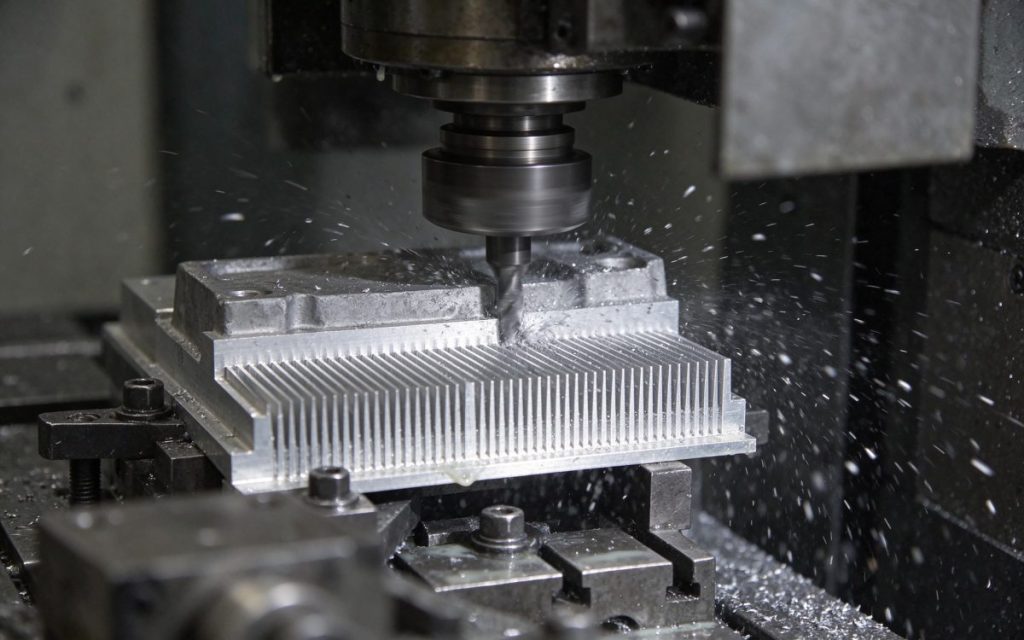
The extruded profile arrives with a wavy mounting face and fins that are already close to finished width. Clamping too hard closes the fins; clamping too light lets the part lift during the face cut.
We used a low-pressure fixture with four soft jaws on the base only, and cut the mounting face in two light passes rather than one heavy pass. The fin roots were cleaned with a 6 mm cutter at a shallow depth so the fins kept their section.
Flatness stayed inside 0.04 mm across 6,000 parts per month, and the shop no longer needs a separate lapping step before assembly.
| Item | Specification | Tolerance | Check |
|---|---|---|---|
| Part size | 180 × 120 × 22 mm | ±0.2 mm | Every part |
| Base flatness | 0.04 mm over full face | 0.05 mm max | 1 in 20 |
| Fin pitch | 4.0 mm, section 1.2 mm | ±0.05 mm | First article |
| Mounting holes | 4 × M6, position from datum A/B | ±0.1 mm | Every part (gauge) |
| Surface finish | Ra 1.6 on base face | Ra 1.6 max | 1 in 50 |
| Cycle time | 3 min 40 s per part | — | Per batch |
The two light passes on the base face are what hold the flatness. One heavy pass pushed the part off the fixture and the fins closed up; splitting the cut keeps the clamping load low and lets the extrusion relax between passes.
MORE CASES
Electronics
Small aluminium connector shells with three bores each — 24 parts on one plate, tapped in the same cycle.
Read case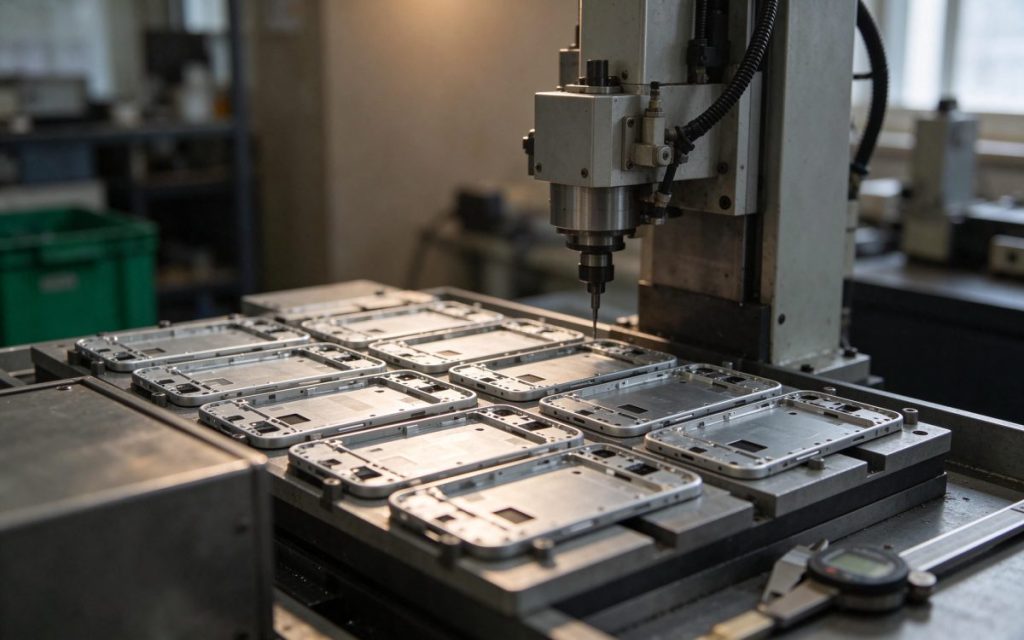
Electronics
Thin-walled aluminium frames with 46 tapped holes each — run on a compact drilling and tapping centre with a repeatable fixture and a fast tool change.
Read case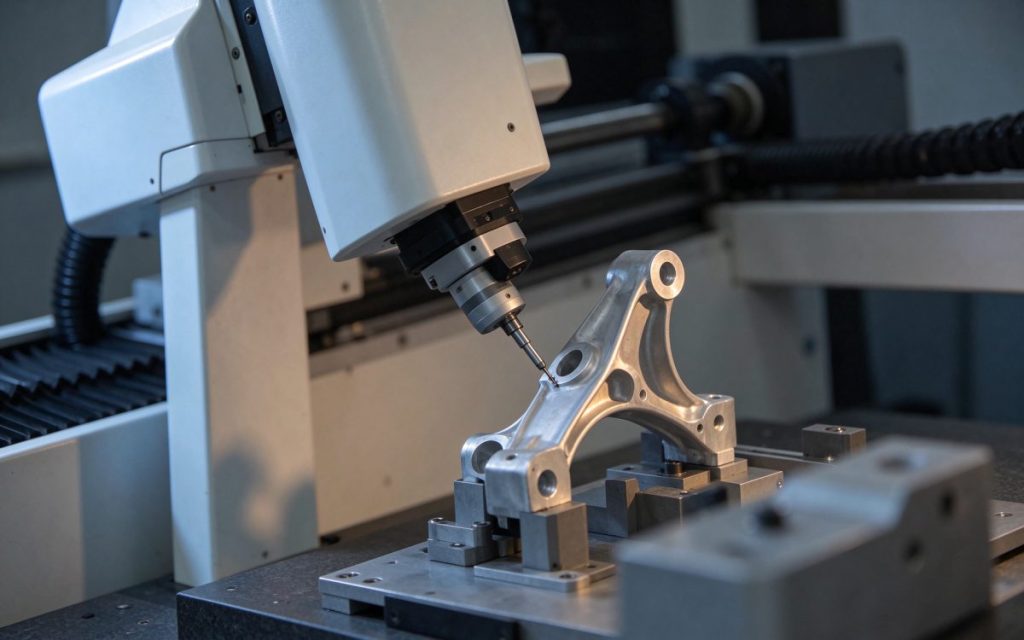
Automotive
A CMM station beside the cell that turned first-article inspection from a two-day wait into a 20-minute check.
Read caseTECHNICAL DATA SHEET
Series datasheet · PDF, 1 page
Tell us where to send follow-up questions and the PDF opens immediately. No newsletter, nothing shared.
Used to follow up on this request only. See our privacy policy.