Automotive
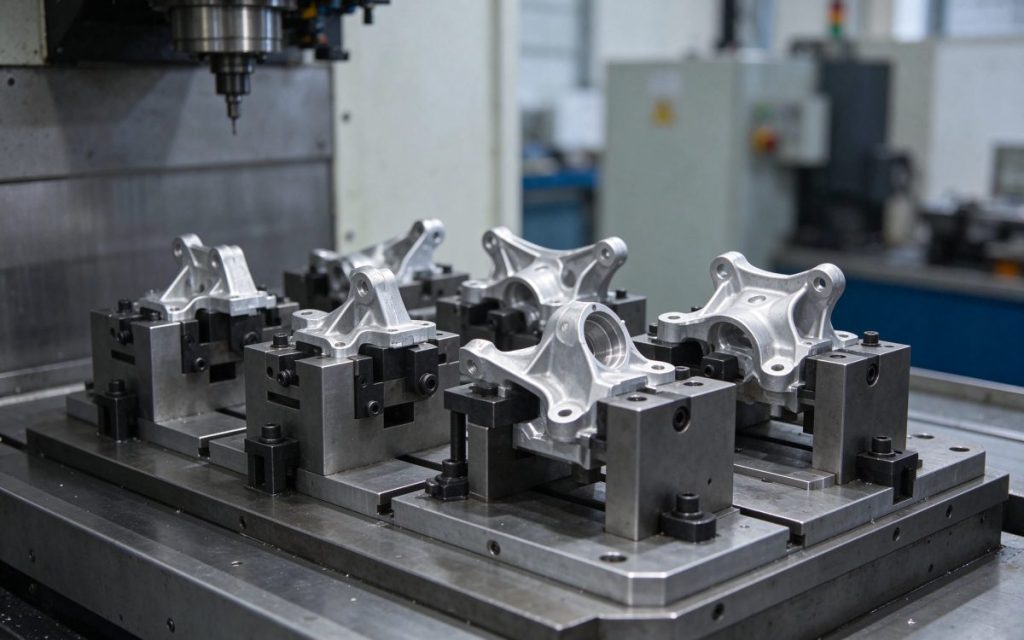
Valve bodies, four-up fixture on a VMC
A four-station fixture that turned a single-part valve body job into a four-part cycle, with the operator loading outside the machine.
Read caseCASE STUDY Automotive
A 420 mm hydraulic piston rod that used to travel between a lathe and a mill now comes off a turn-mill centre complete, thread and flats included.
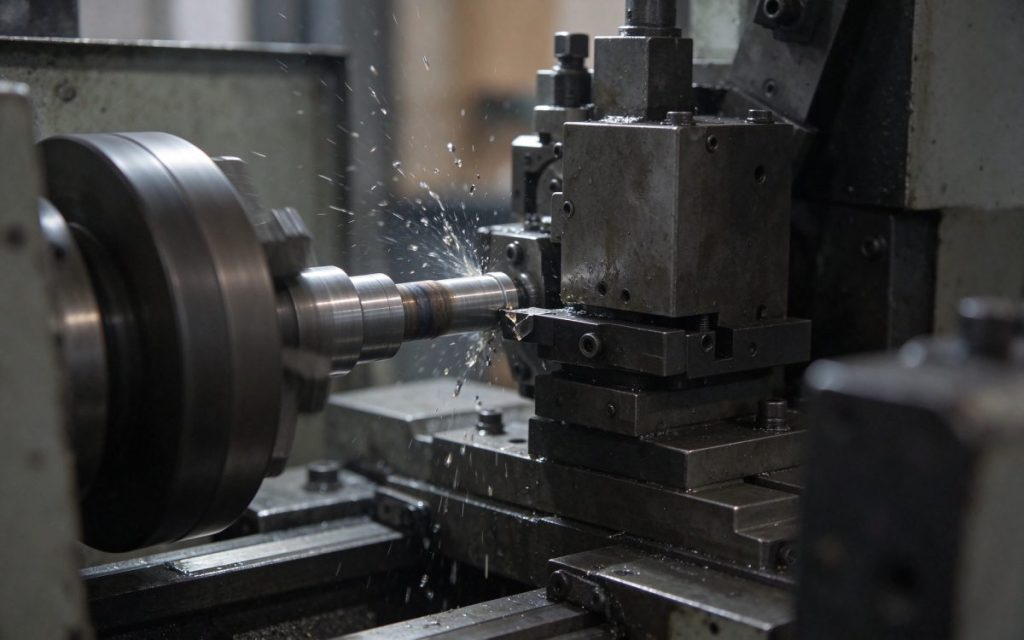
The rod needed turning, a thread at one end, two milled flats and a cross hole. Moving it from the lathe to the mill meant a second clamping and a runout check on every part.
The turn-mill centre does all of it in one clamping: the Y-axis handles the flats, and the cross hole is drilled from the turret before the part is cut off. Runout is set by the chuck, so the check moved to one part per hour.
Cycle time went from 41 to 26 minutes, and the lathe that used to do the roughing now runs a second family of parts.
MORE CASES
Automotive
A four-station fixture that turned a single-part valve body job into a four-part cycle, with the operator loading outside the machine.
Read case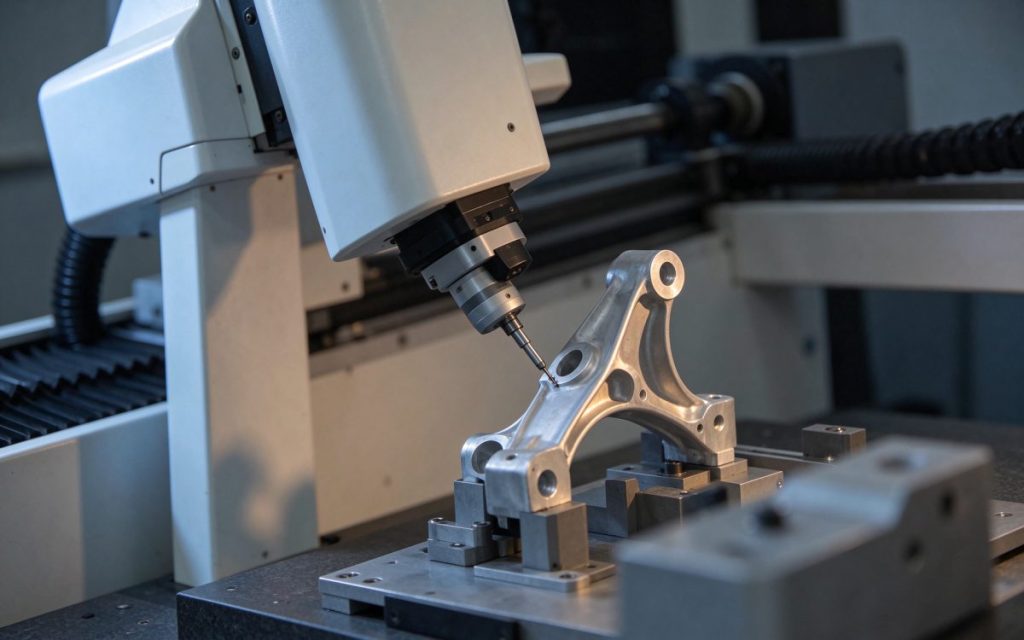
Automotive
A CMM station beside the cell that turned first-article inspection from a two-day wait into a 20-minute check.
Read case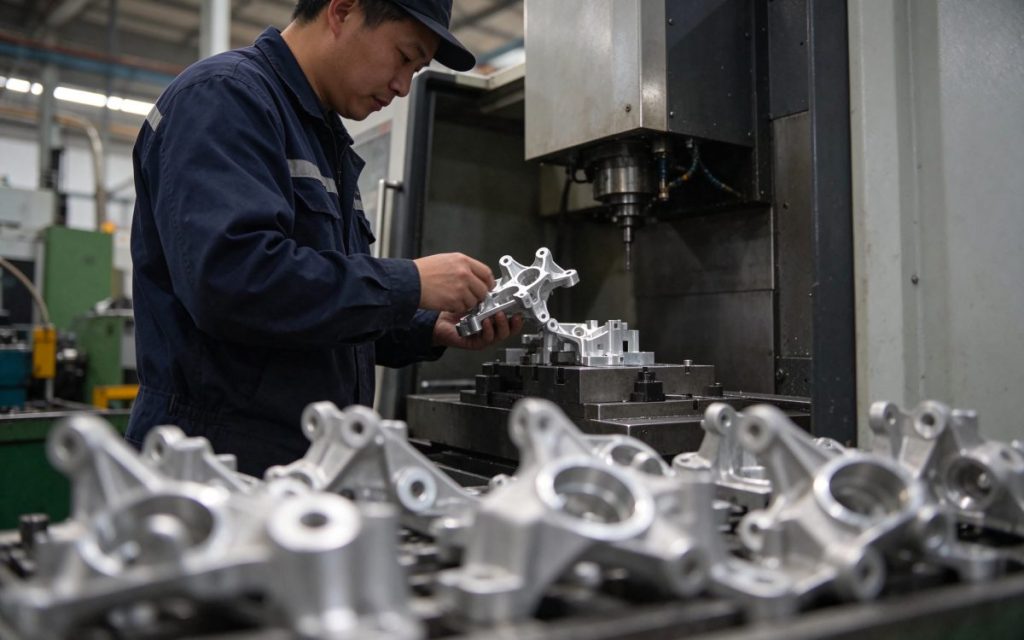
Automotive
An aluminium steering knuckle that used to need two setups now leaves one vertical machining centre complete, with hole position held across the batch.
Read caseTECHNICAL DATA SHEET
Series datasheet · PDF, 1 page
Tell us where to send follow-up questions and the PDF opens immediately. No newsletter, nothing shared.
Used to follow up on this request only. See our privacy policy.