Mould & die
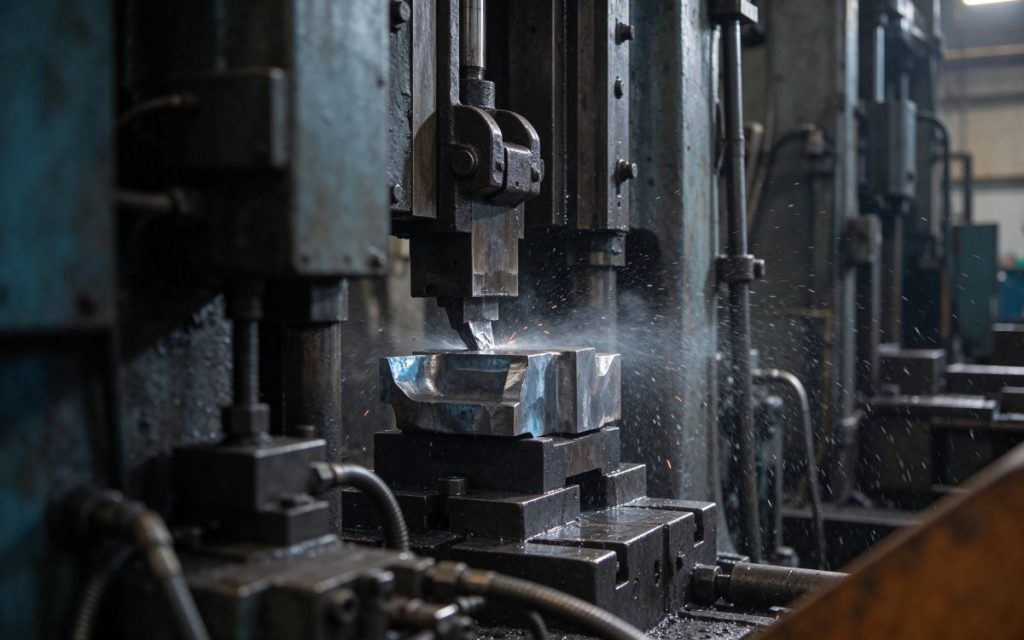
Die inserts finished to a 0.02 mm parting line
Hardened die inserts that used to be ground after milling now come off the machine with the parting line inside tolerance.
Read caseCASE STUDY Mould & die
Eight steel flanges with six bolt holes each, drilled and countersunk in a single cycle on a vertical drilling machine.
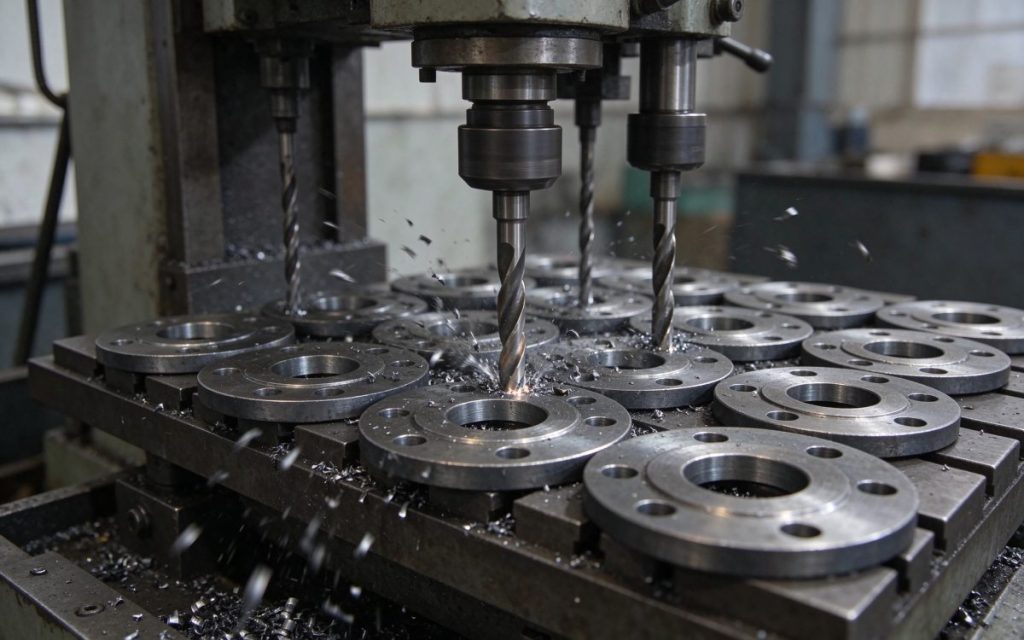
These flanges are plain parts, but there are a lot of them and every hole has to line up with the mating pipe. Radial drilling one hole at a time was both slow and inconsistent.
The machine is set up with a four-spindle head and a fixture holding eight flanges. Two indexes cover all six holes plus the countersink, with the positions taken from the fixture rather than from a marked-out plate.
Hole position now holds at ±0.1 mm, and the shop runs 1,200 flanges a month in the time it used to take for 700.
MORE CASES
Mould & die
Hardened die inserts that used to be ground after milling now come off the machine with the parting line inside tolerance.
Read case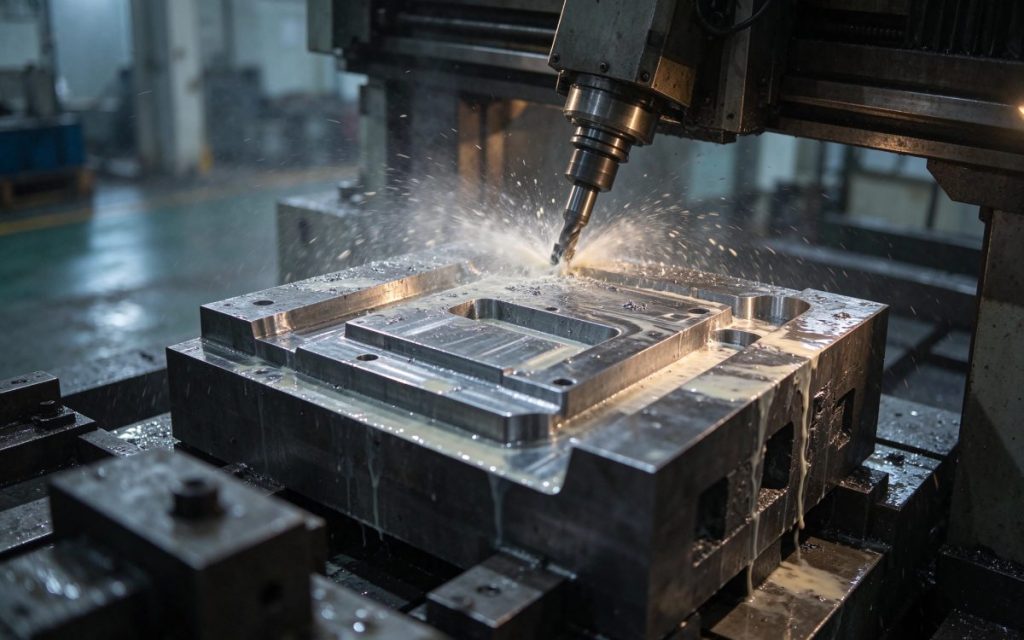
Mould & die
A 1.2-tonne mould core where roughing and finishing now happen on the same gantry machine, with the contour left to a single finishing pass.
Read case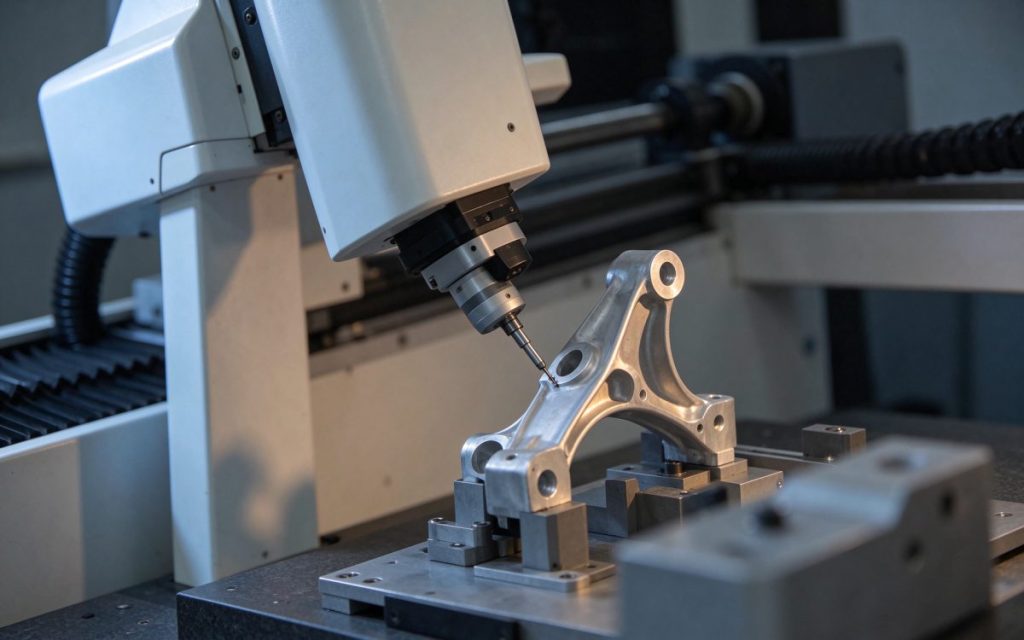
Automotive
A CMM station beside the cell that turned first-article inspection from a two-day wait into a 20-minute check.
Read caseTECHNICAL DATA SHEET
Series datasheet · PDF, 1 page
Tell us where to send follow-up questions and the PDF opens immediately. No newsletter, nothing shared.
Used to follow up on this request only. See our privacy policy.