Electronics
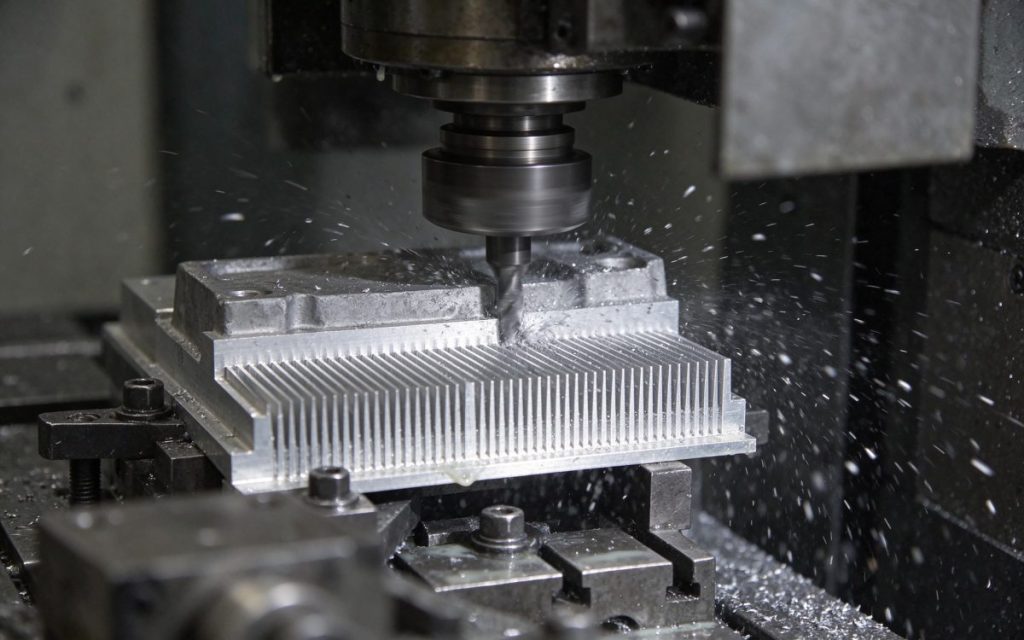
Heatsink base plates, fins machined in one pass
A 180 × 120 mm extruded heatsink base needed the fin roots cleaned and the mounting face flat within 0.05 mm — done in one clamping on a vertical mill.
Read caseCASE STUDY Electronics
Thin-walled aluminium frames with 46 tapped holes each — run on a compact drilling and tapping centre with a repeatable fixture and a fast tool change.
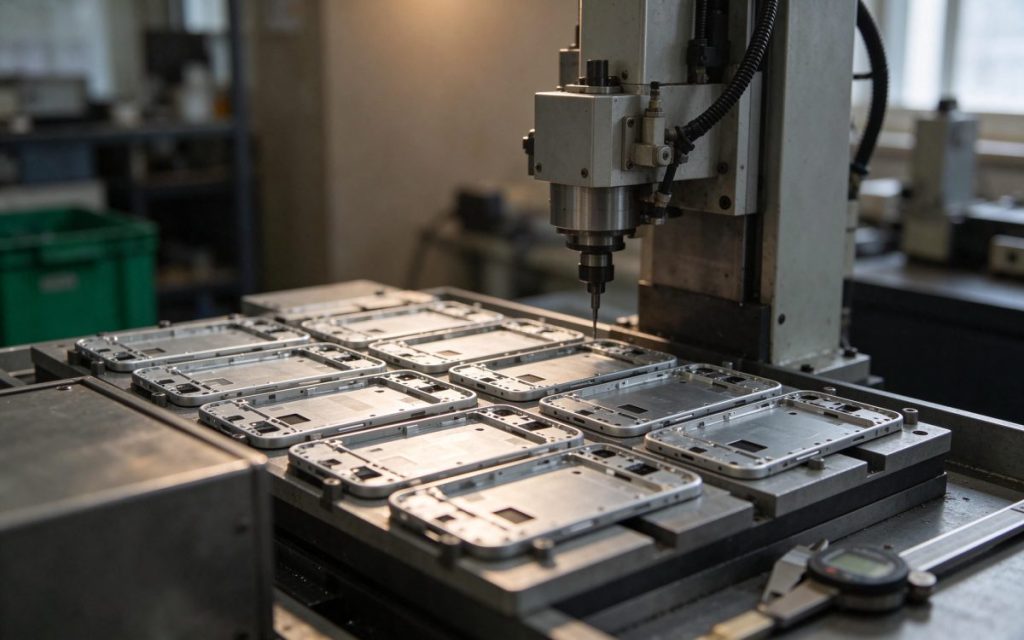
Each frame carries 46 small tapped holes and two machined pockets, with a 1.2 mm wall that cannot take much clamping force. On the previous setup, thin walls deflected under the vise and the tap broke roughly once every 300 parts.
The fixture was rebuilt with a vacuum plate plus four light clamps, and the cycle was split so the walls are machined before the tapping operation. Spindle speed, feed and peck depth for the M1.6 taps were set from trials on the customer material rather than from a chart.
Scrap fell from 3.1% to 0.9% in the first month, and tap consumption dropped enough to pay for the fixture in eleven weeks.
MORE CASES
Electronics
A 180 × 120 mm extruded heatsink base needed the fin roots cleaned and the mounting face flat within 0.05 mm — done in one clamping on a vertical mill.
Read case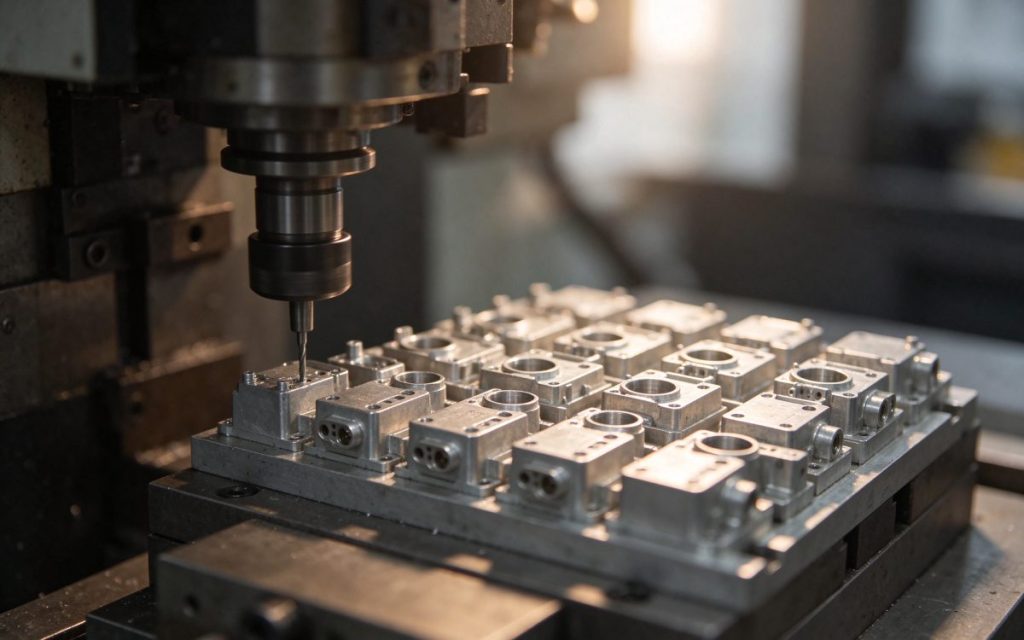
Electronics
Small aluminium connector shells with three bores each — 24 parts on one plate, tapped in the same cycle.
Read case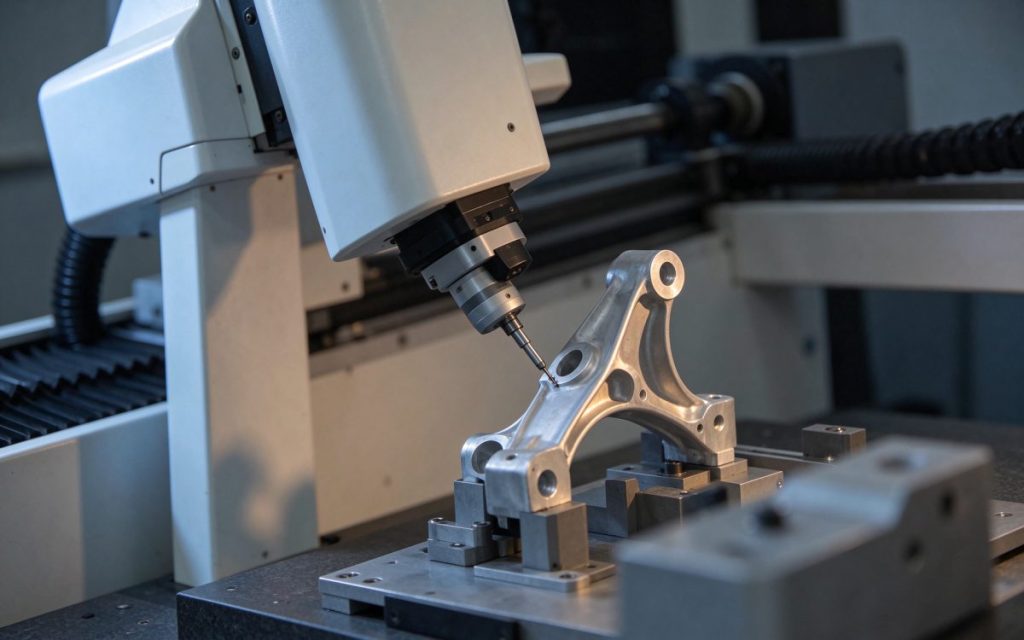
Automotive
A CMM station beside the cell that turned first-article inspection from a two-day wait into a 20-minute check.
Read caseTECHNICAL DATA SHEET
Series datasheet · PDF, 1 page
Tell us where to send follow-up questions and the PDF opens immediately. No newsletter, nothing shared.
Used to follow up on this request only. See our privacy policy.